‹
›
‹
›
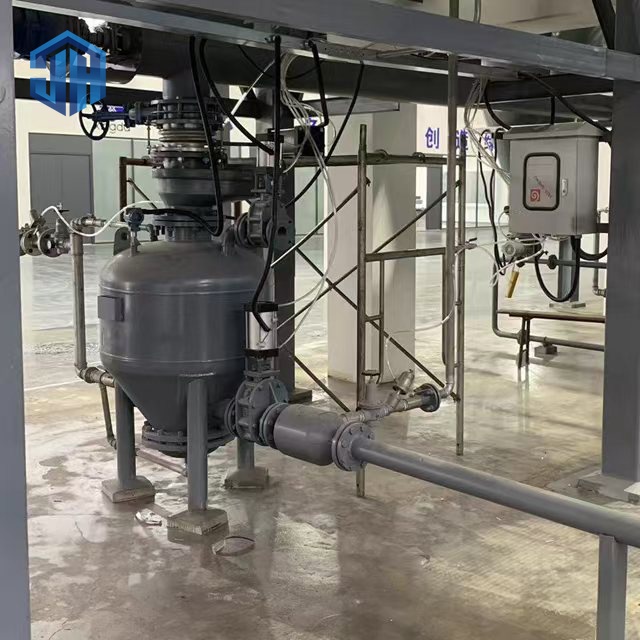
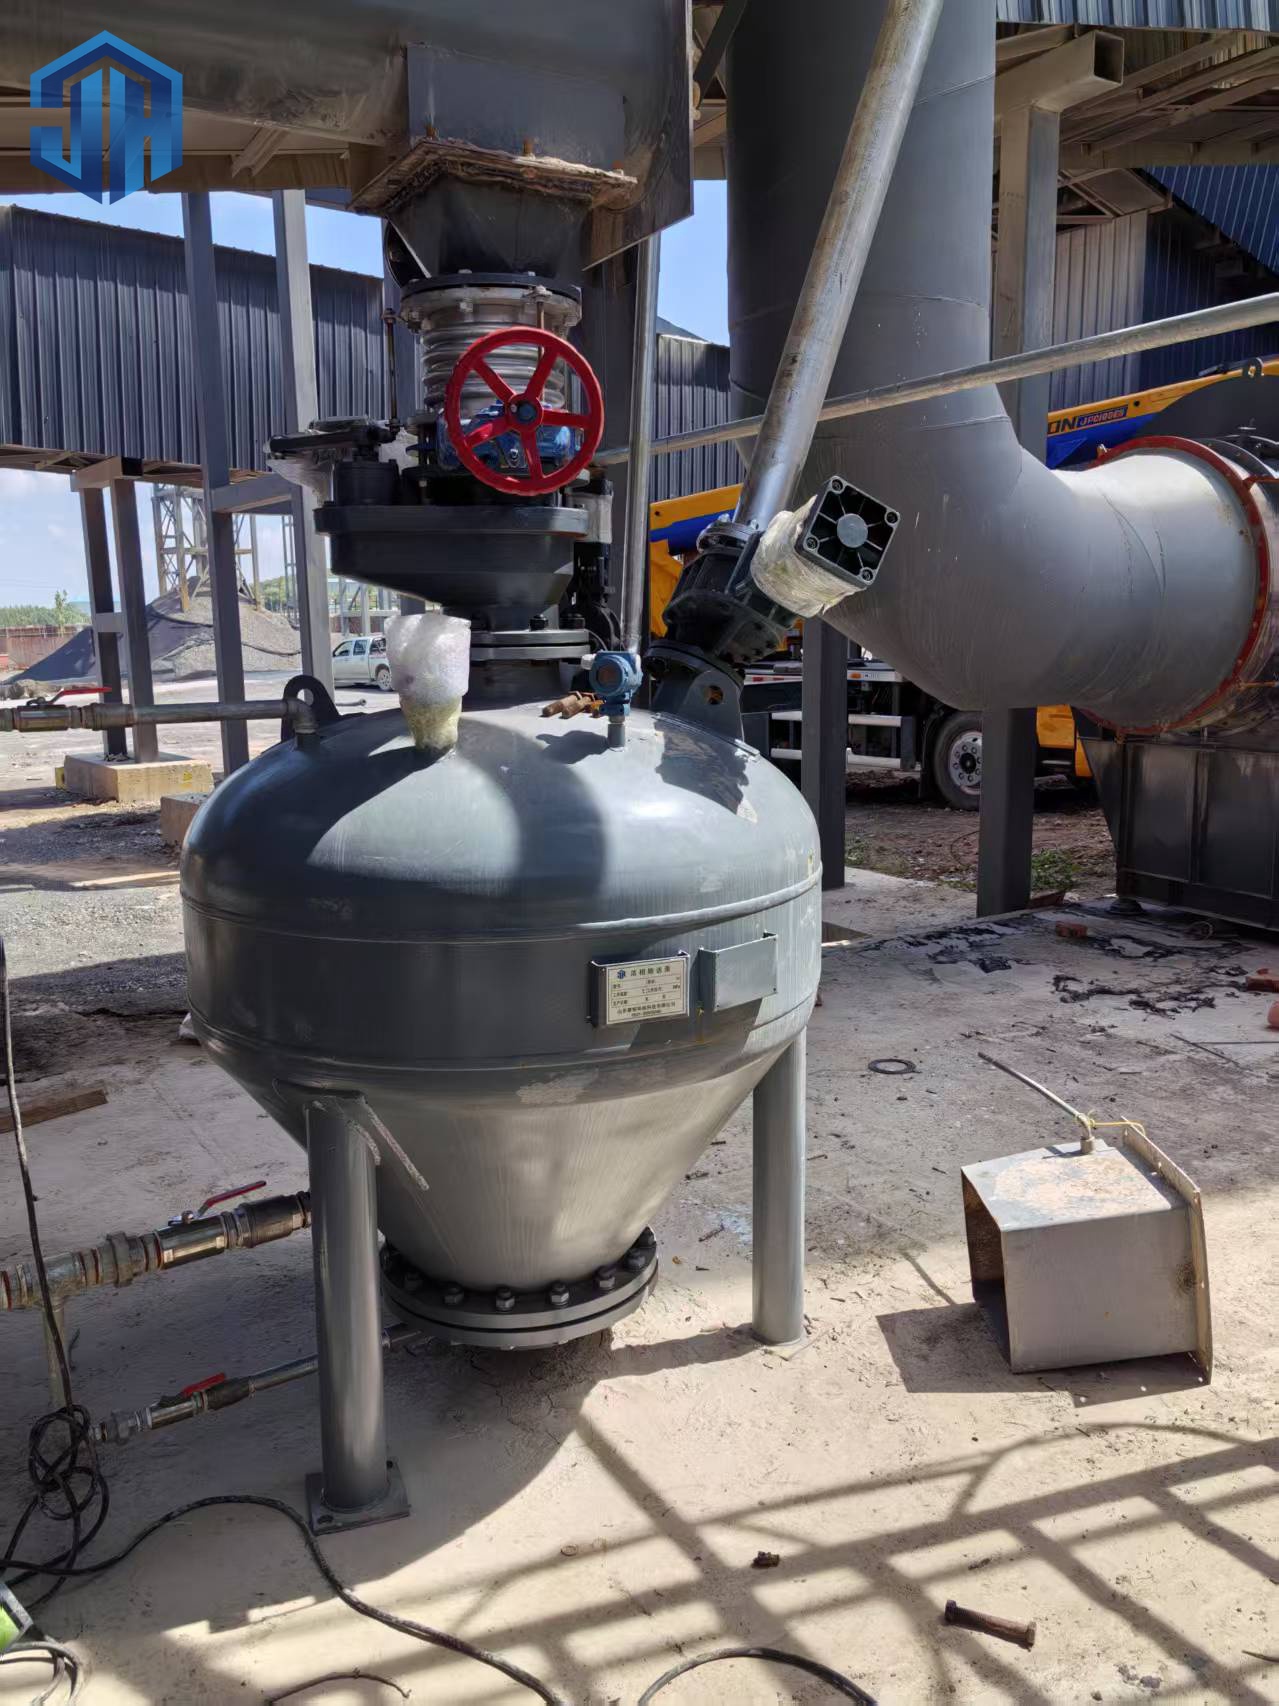
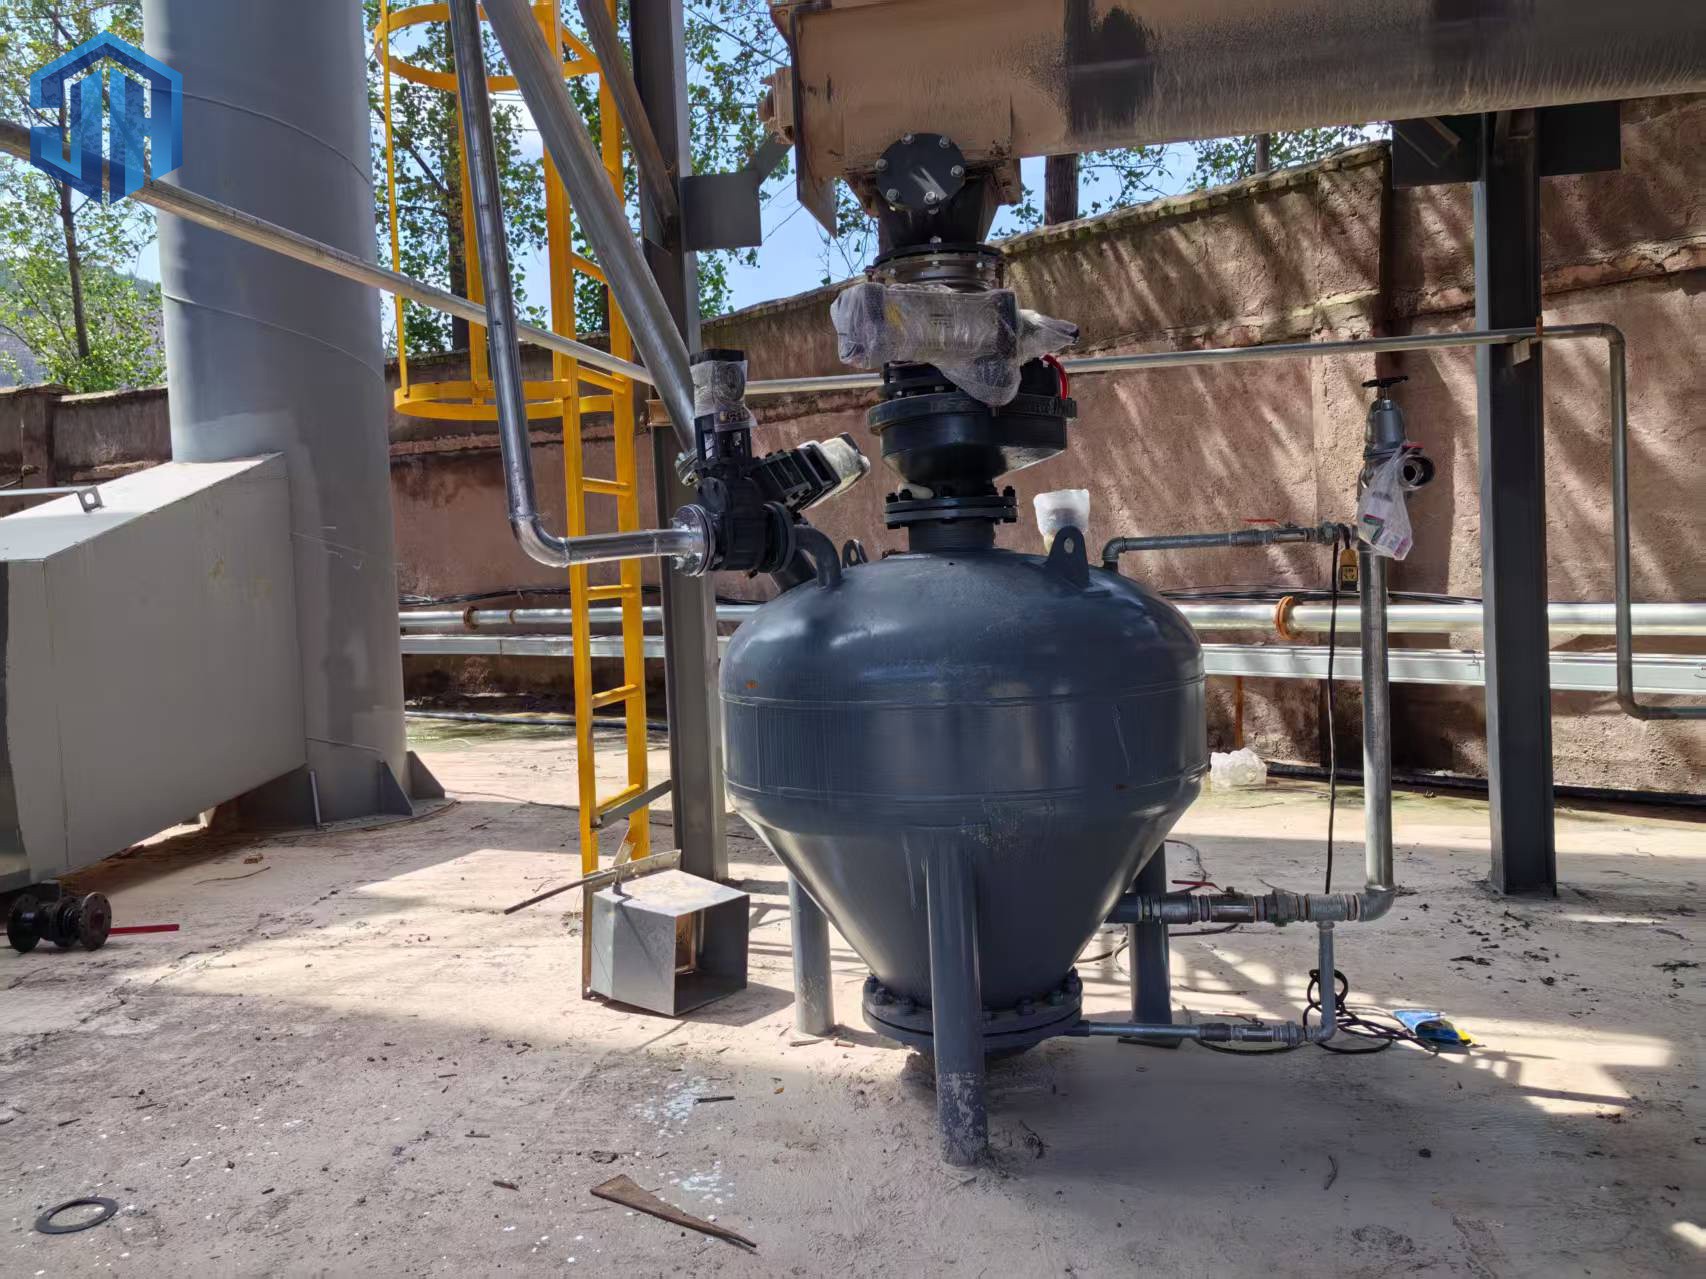
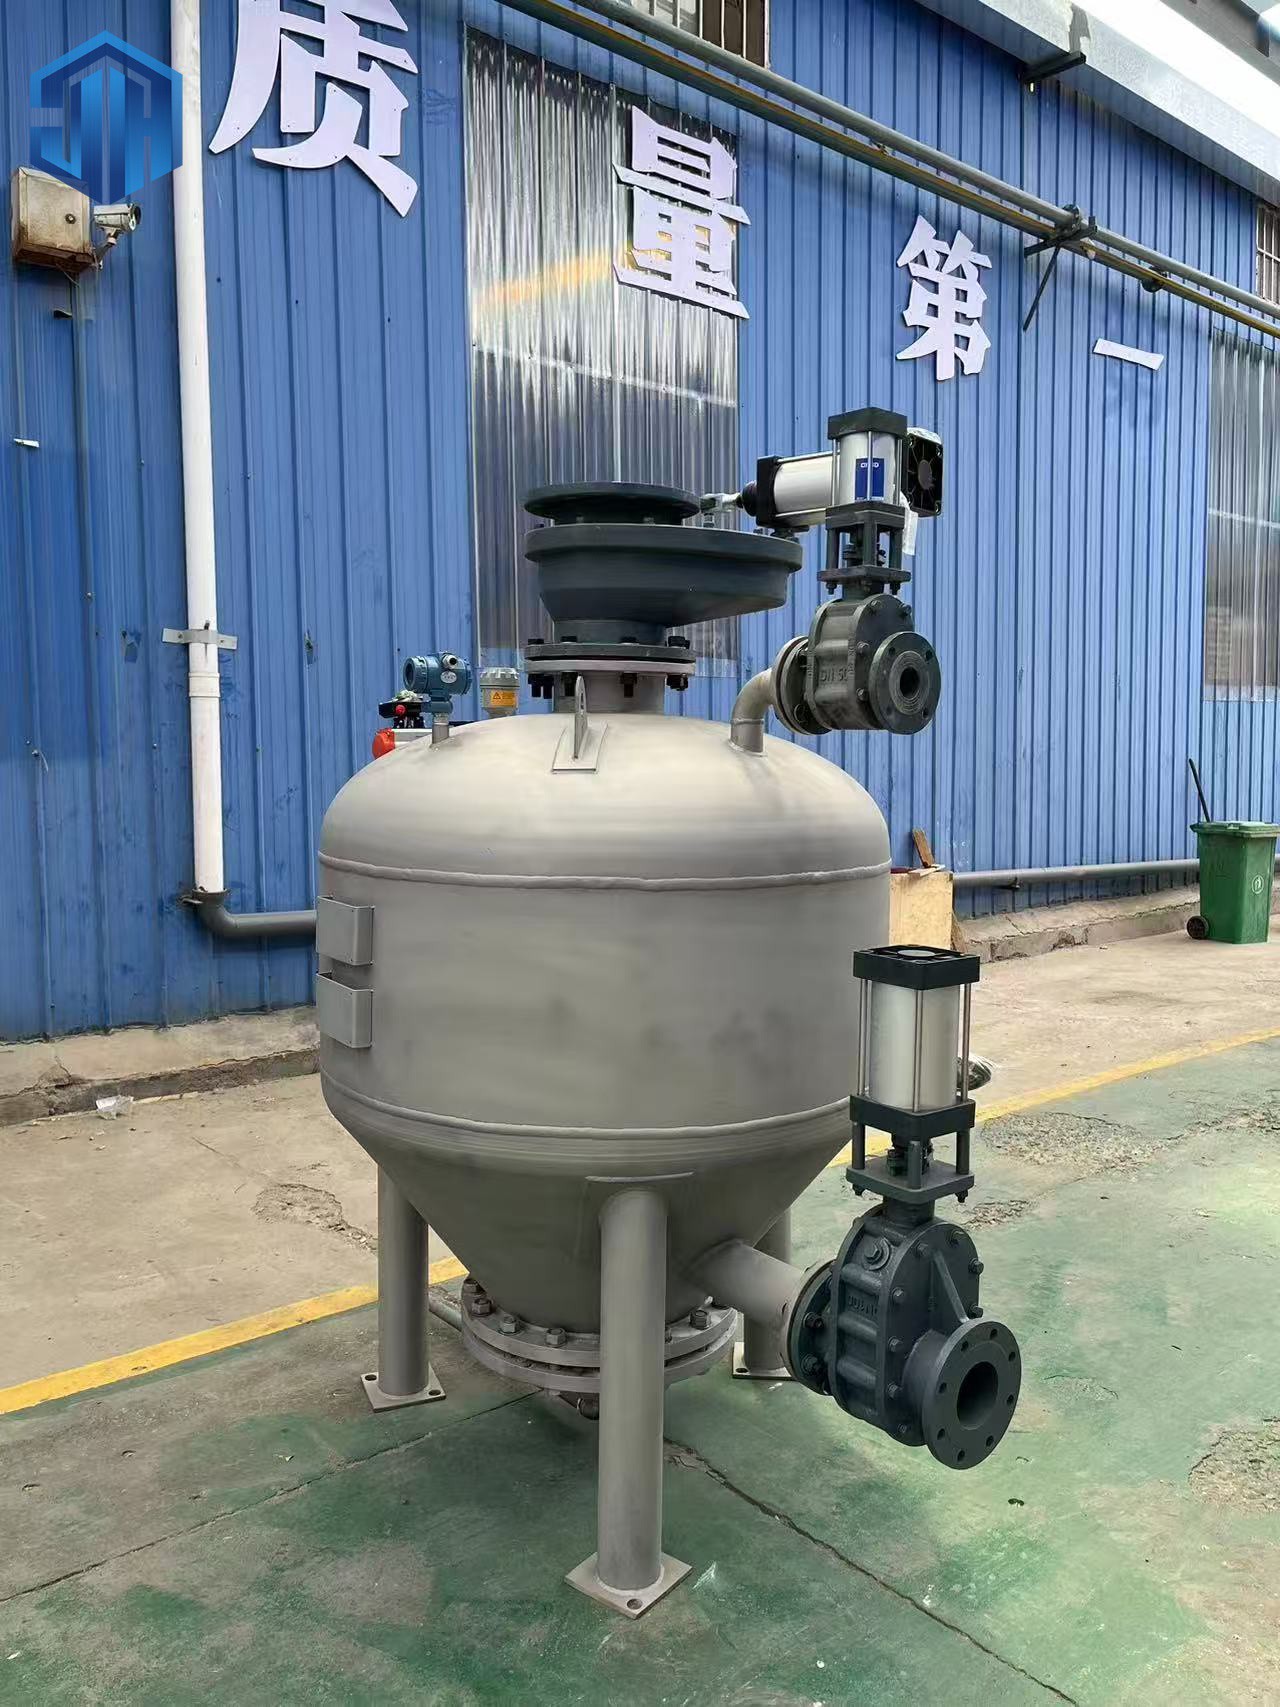
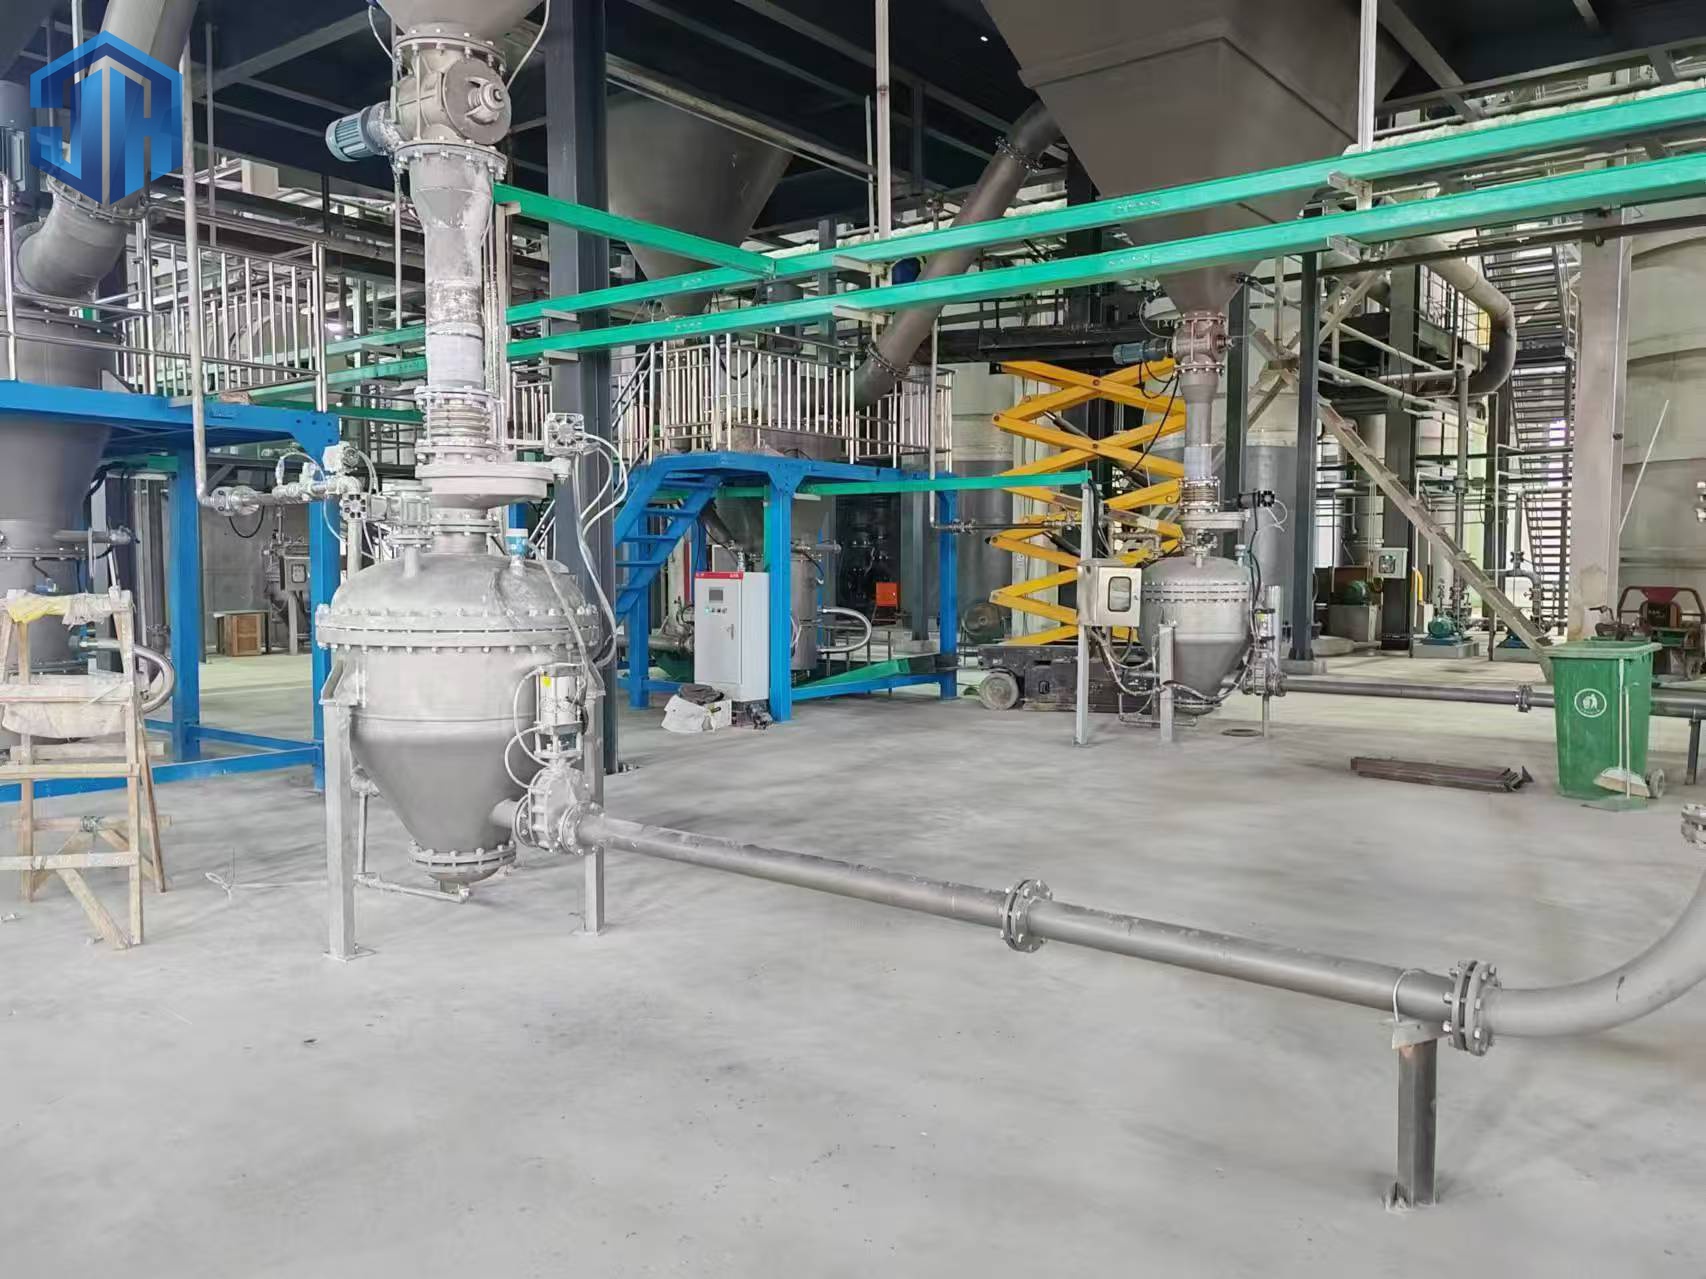
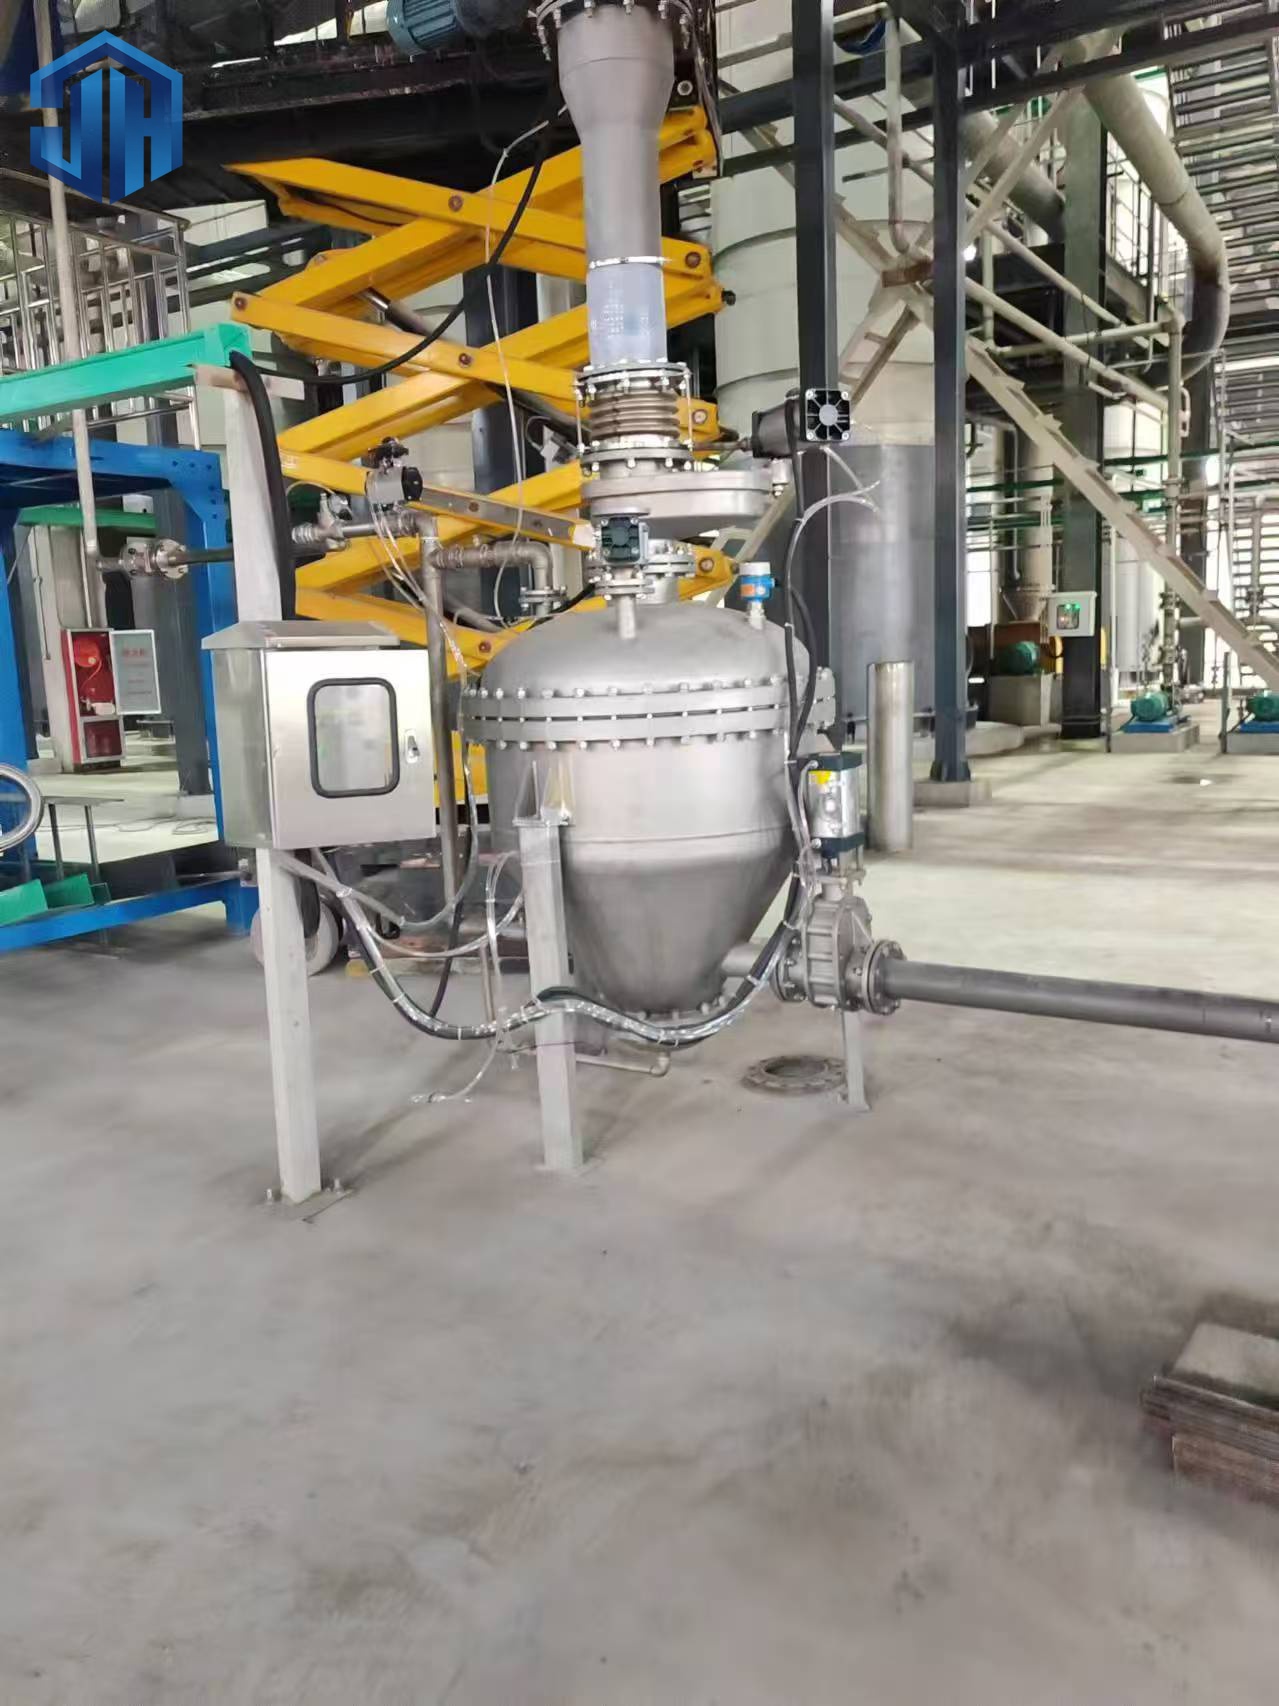
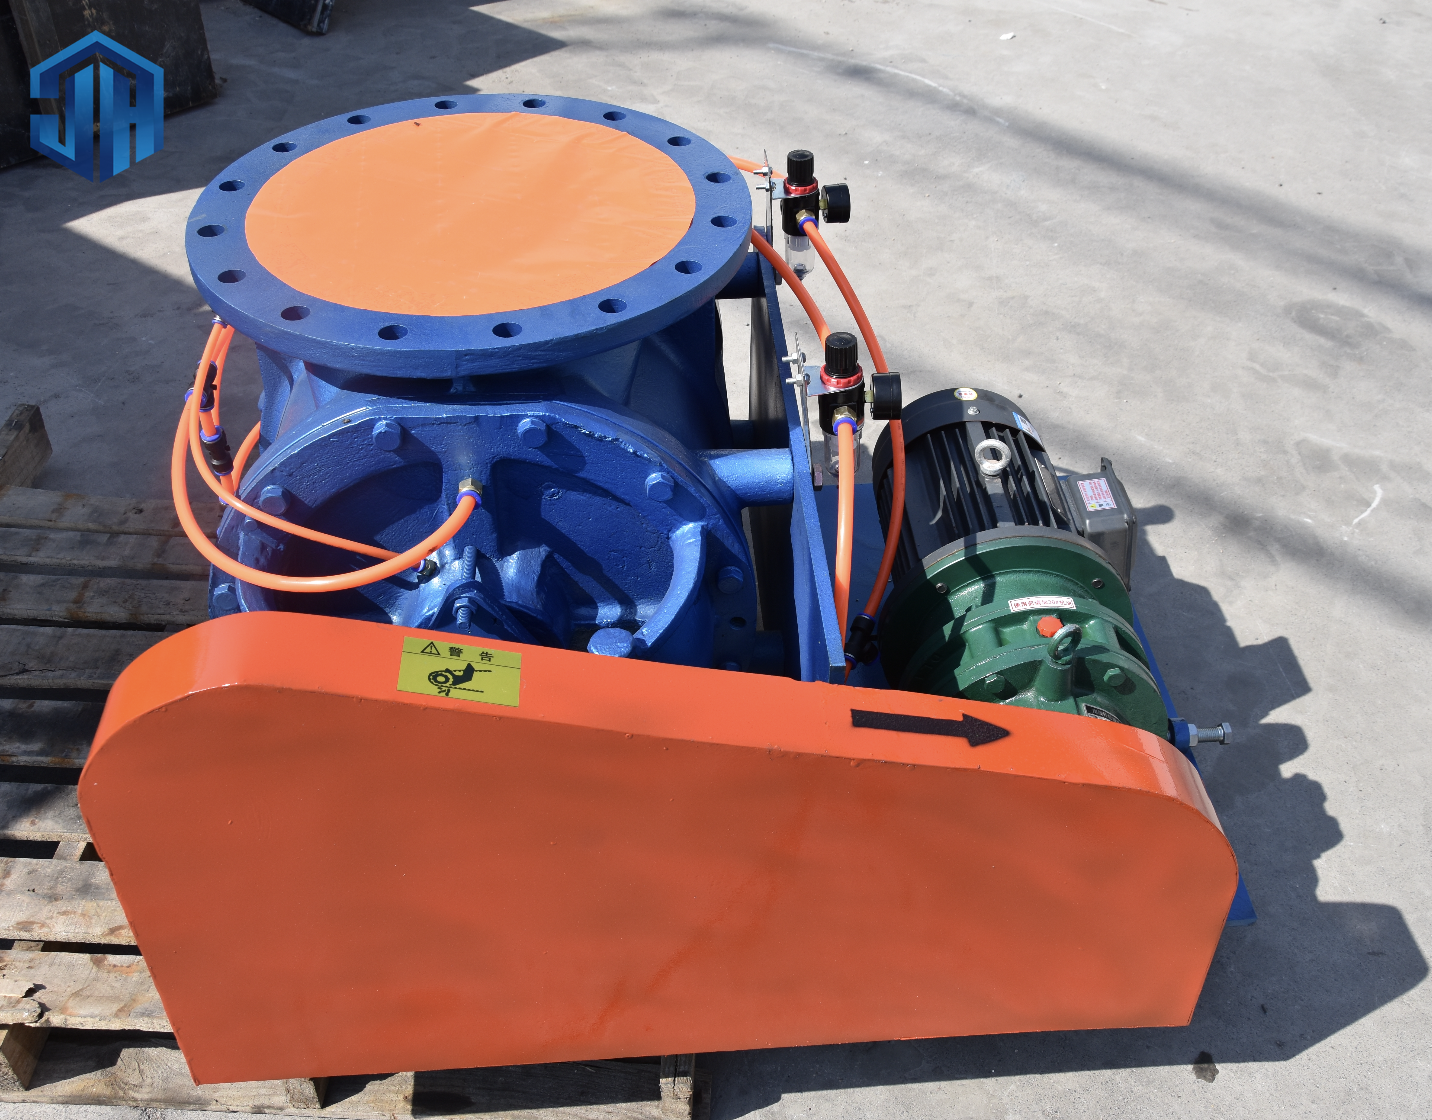
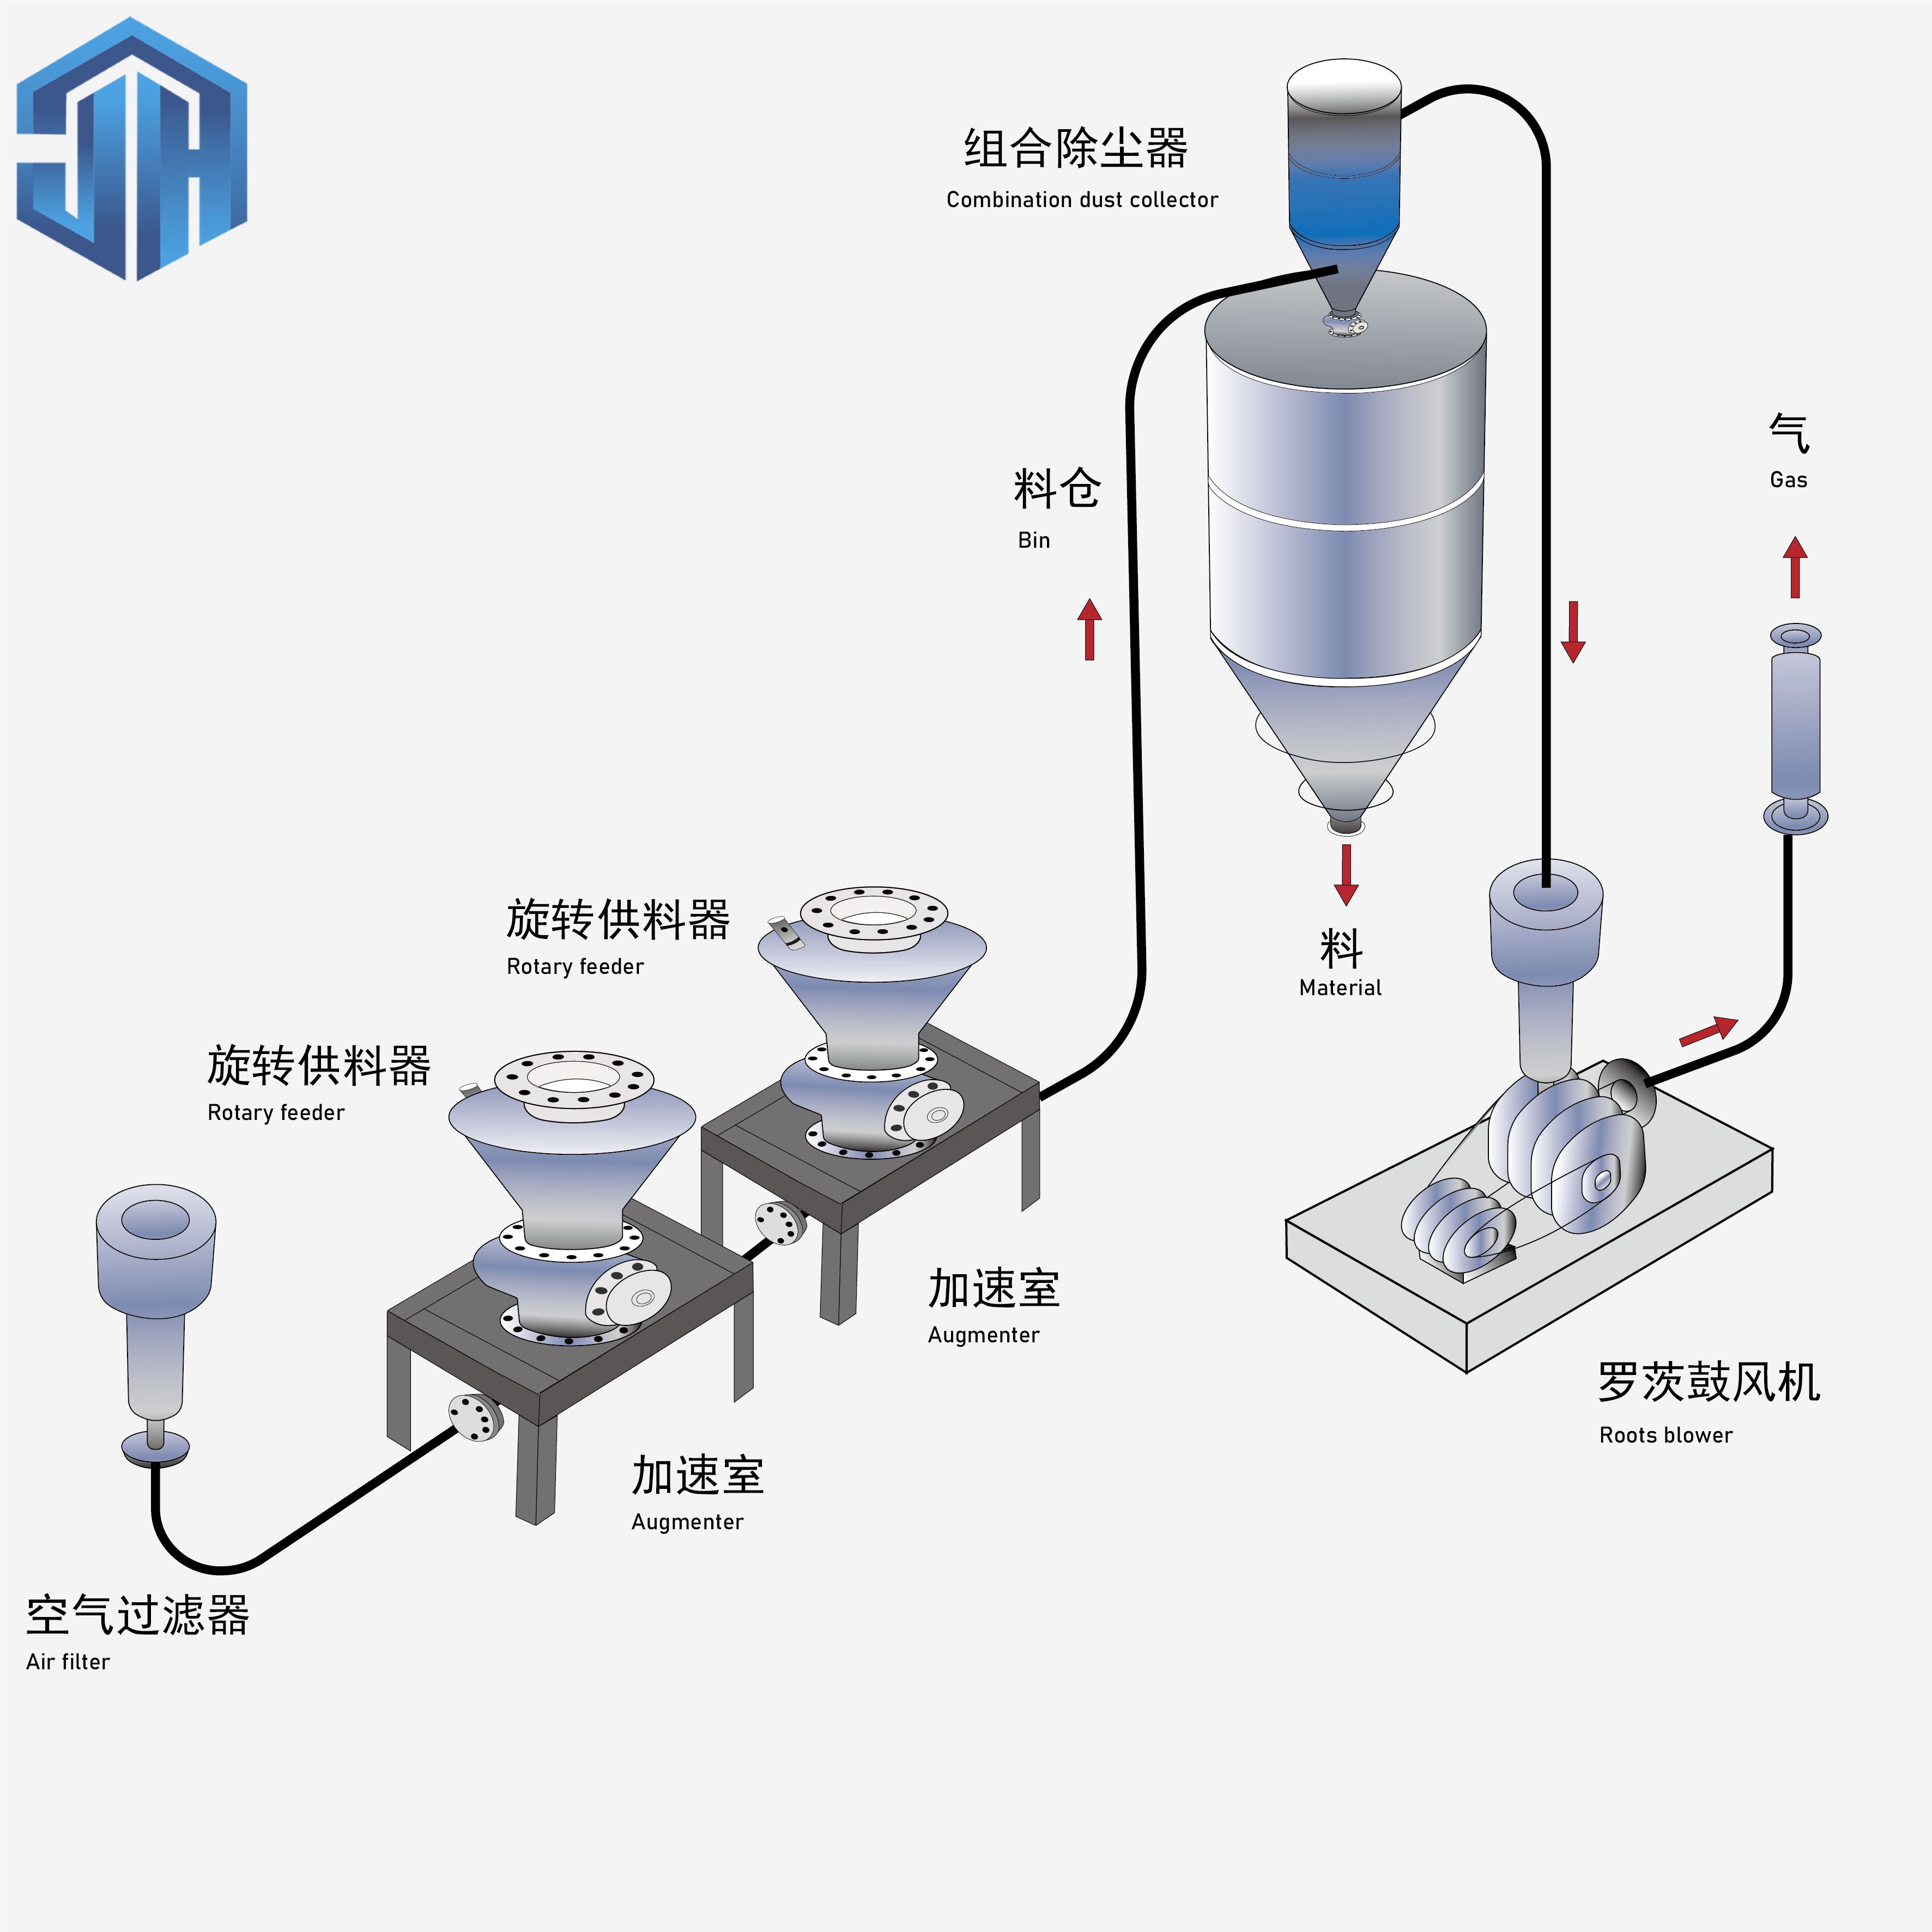
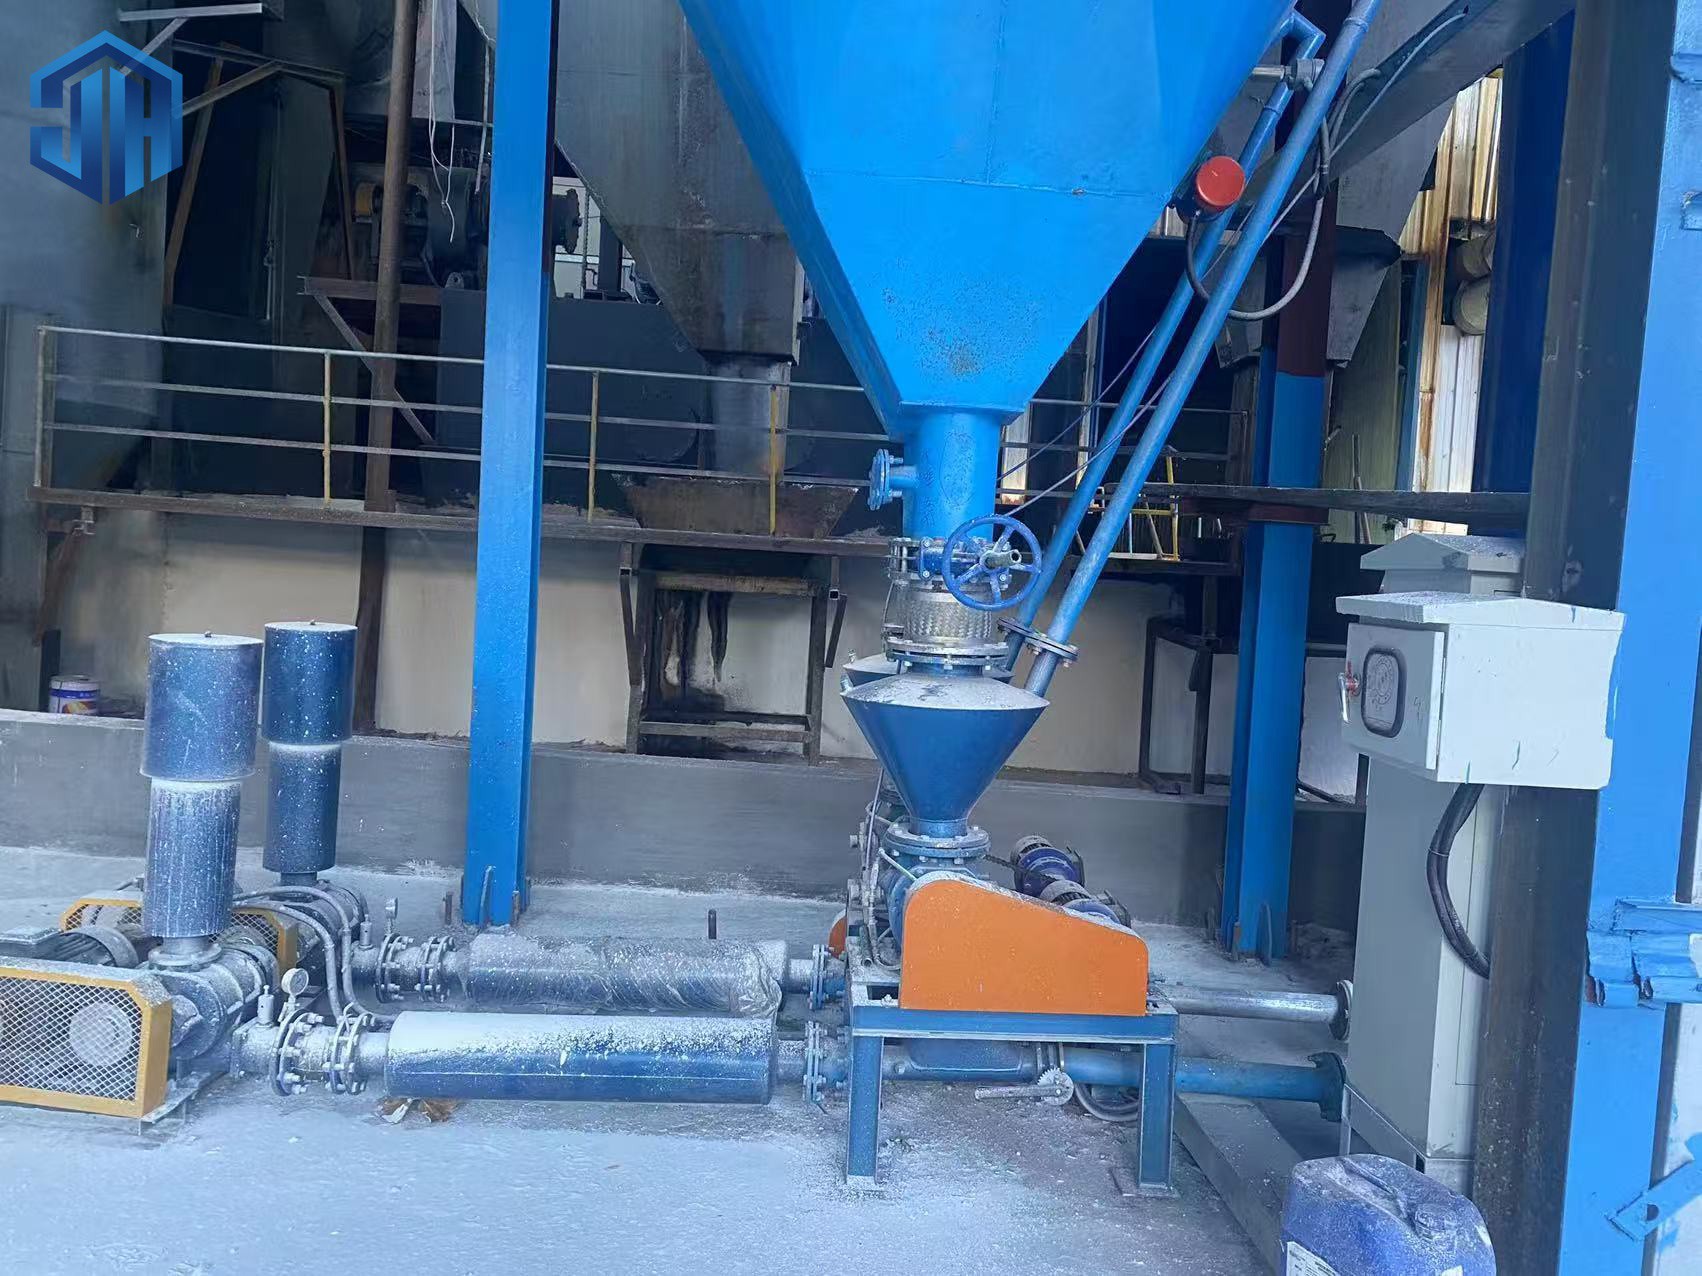
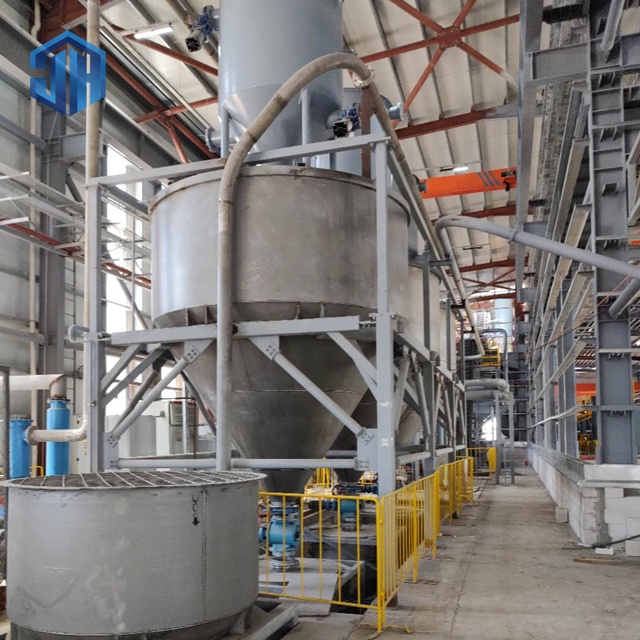
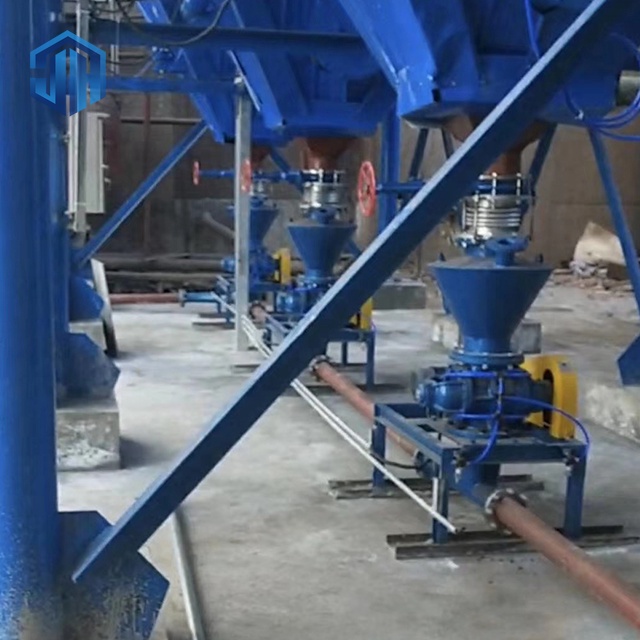
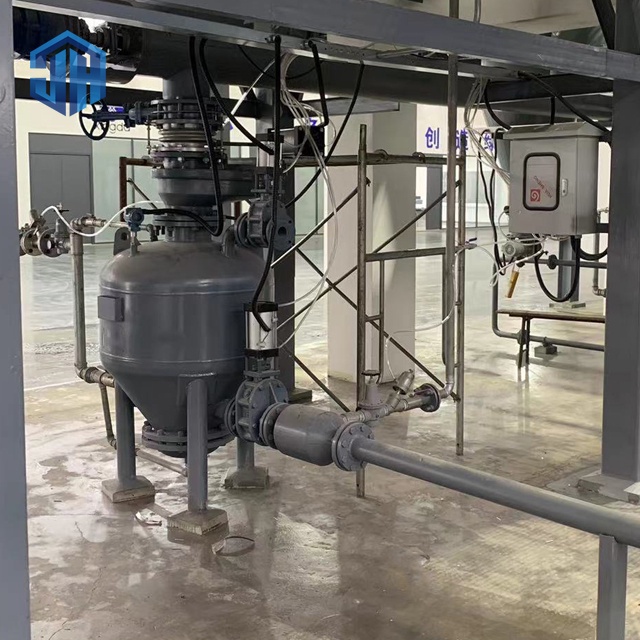
The bin pump adopts positive pressure pneumatic conveying to transport powdered materials. In the positive pressure dense-phase plug flow conveying system, it does not generate power itself. Instead, it relies on externally supplied compressed air to mix and pressurize the powdered materials loaded into the pump, which are then transported to the ash silo through pipelines.
It is widely used for the conveyance of materials such as fly ash, cement, cement raw materials, and mineral powder in power plants. With a working pressure ranging from 0.1 to 0.6 MPa (depending on the conveying distance), it can operate at temperatures from -20℃ to 400℃, meeting the challenges of higher temperatures. It is also capable of conveying powder over long distances.
The conveying pipeline can be flexibly arranged according to topographical conditions, enabling centralized, decentralized, high-altitude, and long-distance conveying. The conveying process is not affected by natural conditions, ensuring that the material is not affected by moisture, and it is environmentally friendly and pollution-free. Therefore, bin pump conveying has the advantages of long conveying distance, low gas velocity, high solid-to-gas ratio, low energy consumption, low gas consumption, minimal pipeline wear, less material breakage, easy dust removal, high automation level, and broad application prospects.
This equipment adopts a PLC control system, allowing for automatic or manual control. After long-term practical operation, it has been proven to have stable performance, reliable quality, and affordability. It ensures dust-free conveying, making it an ideal pneumatic conveying device.
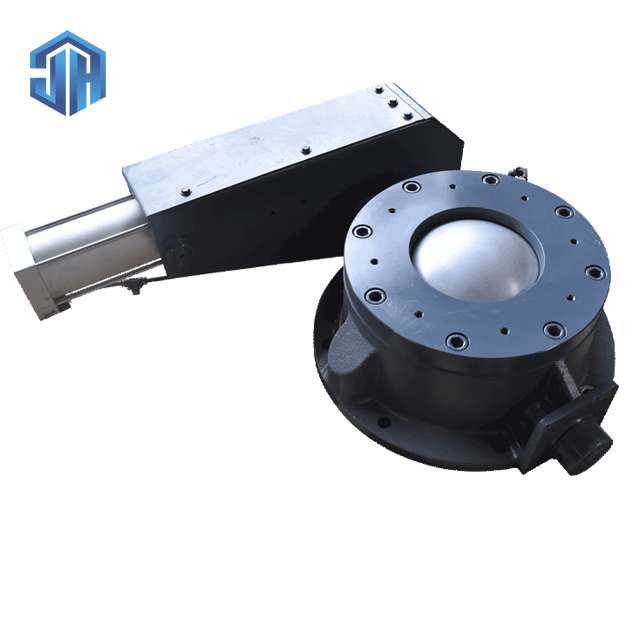
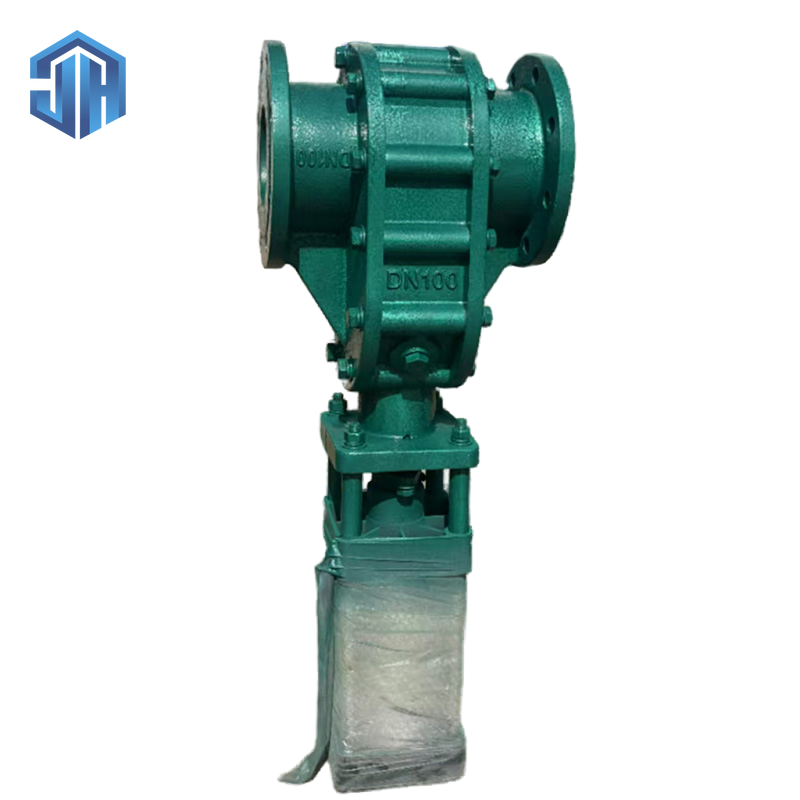
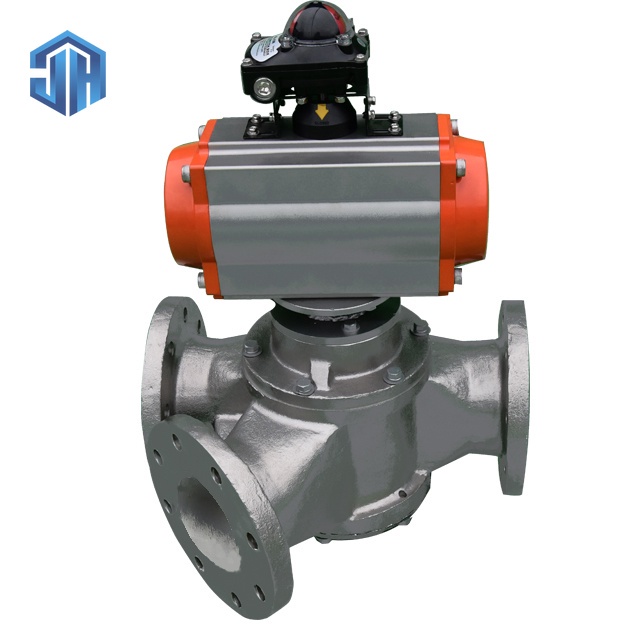
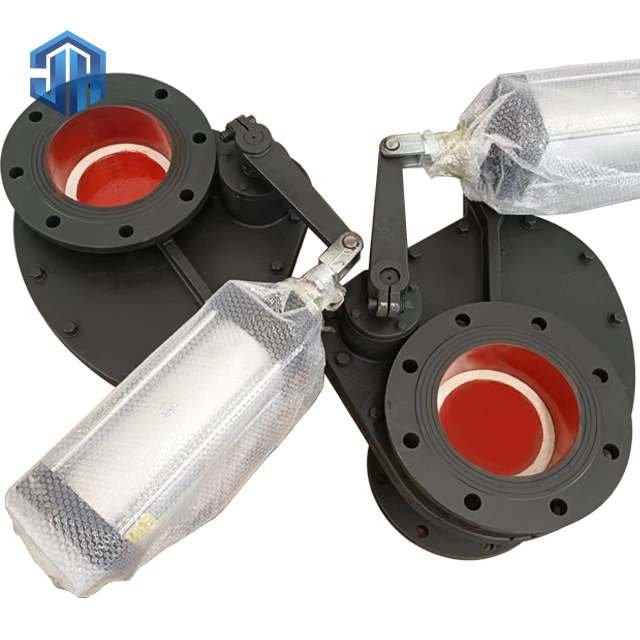
It primarily consists of five major components: a dense-phase bin pump, pneumatic valves, a compressed air source, a control system, conveying pipes, and an ash silo.
- Q : How can I get the price?A : We usually quote within 12 hours after we get your inquiry.
- Q : Can I buy samples? - Yes. Please feel free to contact us.A : Our MOQ: 1 SETS
- Q : What is your delivery time?A : It depends on the order quantity,as general with 15 days.
- Q : What is your payment term?A : T/T, CASH.L/C,Western Union, MoneyGram, and Paypal. This is negotiable.
Contact Us
If you have any cooperation intentions or product questions, please leave us a message!
We will get back to you as soon as possible!
Please give us a message